
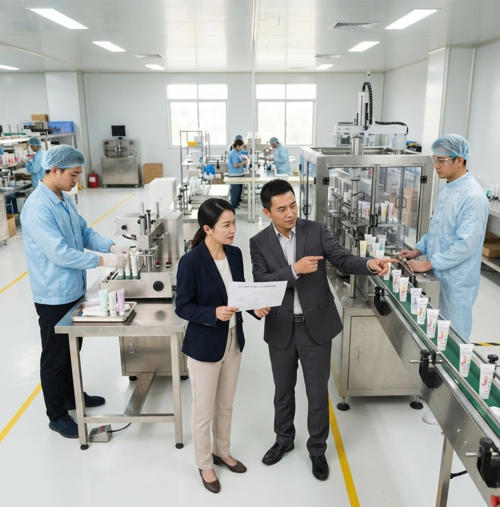
Why the Right Ultrasonic Sealing Machine Is Critical to Your Success
Sealing integrity is not just a packaging specification. It is a direct determinant of product safety, shelf-life performance, brand reputation, and regulatory standing. A tube that reaches a retail shelf with a compromised seal is a customer complaint, a potential recall trigger, and — in pharmaceutical markets — a documented defect in a regulated product.
Choosing the wrong sealing machine for your production context creates problems that compound quietly: inconsistent seal quality that looks acceptable at visual inspection but fails under distribution pressure, thermal degradation of heat-sensitive formulations, compliance gaps that surface during audits rather than during machine evaluation, and changeover complexity that turns a 30-minute format switch into a 2-hour production disruption.
This guide walks you through every dimension of a rigorous ultrasonic tube sealing machine selection — from tube material compatibility and production speed matching, through compliance requirements and total cost of ownership, to the specific questions that separate vendors with genuine application experience from those with a well-designed brochure.

The sealing station is the last quality gate before your product enters the distribution chain. Getting the machine specification right determines whether that gate is a reliability asset or a liability.
Understand Your Tube Material: The Foundation of a Perfect Seal
Ultrasonic sealing works by transmitting high-frequency mechanical vibrations through the tube tail, generating heat at the molecular interface between the inner tube wall layers. That process depends entirely on the tube material’s ability to absorb and transmit ultrasonic energy — and different tube constructions respond differently.
Specifying a sealing machine without confirming material compatibility first is the most common — and most expensive — mistake in tube sealing equipment selection.
| Tube Material | Ultrasonic Compatibility | Key Specification Notes | Common Application |
|---|---|---|---|
| PE (Polyethylene) — Single Layer | ✅ Excellent | Clean, fast fusion. Typical dwell: 0.5–1.2s. Amplitude: standard. Ideal entry point for ultrasonic sealing. | Toothpaste, body lotions, hand creams, shampoo conditioners |
| PBL (Plastic Barrier Laminate) | ✅ Very Good | Multiple polymer layers each contribute to the bond. Slightly longer dwell time than single-layer PE. Confirm layer count with sonotrode frequency matching. | Premium cosmetic creams, serums, multi-layer cosmetic tubes |
| ABL (Aluminum Barrier Laminate) | ✅ Good — Preferred Method | Aluminum foil layer makes conventional heat sealing risky (delamination). Ultrasonic is the preferred — and often only — viable method. Requires parameter optimization for foil thickness. | Pharmaceutical ointments, antifungal creams, retinol serums |
| PP (Polypropylene) | ✅ Good | Higher melt temperature than PE requires elevated amplitude. Confirm sonotrode power output is adequate for PP wall thickness. | High-clarity cosmetic tubes, premium packaging formats |
| Full-Metal Aluminum Tubes | ❌ Not Compatible | Metallic construction does not support molecular fusion. Hot-jaw or impulse sealing is the correct method for full-metal tubes. | Traditional pharmaceutical ointment tubes |
Before shortlisting any machine, send tube samples from your actual production supply chain to the supplier for material compatibility testing. Wall thickness variation between batches from different tube suppliers can shift the required amplitude by 5–10% — a range that should be within the machine’s adjustable parameters, but must be confirmed, not assumed.
Define Your Production Speed and Output Goals Before Comparing Machines
Every ultrasonic sealing machine has a rated speed, and almost no machine achieves that speed in real production conditions. The number that matters is not the rated speed — it is the sustained throughput at your OEE (Overall Equipment Effectiveness — the ratio of actual productive output to theoretical maximum, typically 75–85% on a well-run packaging line).
📐 The Right Sizing Formula
Calculate your target output per hour, add 20% as a growth buffer, then divide by 0.80 to account for realistic OEE. Example: a 5,000 tubes/hour target becomes a 7,500 tubes/hour rated capacity requirement. A machine rated at 6,000 tubes/hour will be running above comfortable OEE range within 18 months as volume grows — making it a bottleneck, not a solution.
⚡ Semi-Automatic: Under 2,000 tubes/hour
Semi-automatic ultrasonic sealers (operator-loaded, machine-sealed) run 18–30 tubes per minute. Correct for small-batch cosmetic contract operations, specialty pharmaceutical runs, and distributors demonstrating the technology to clients. Investment range: $8,000–$25,000. Upgradeable to automatic configuration on modular platforms.
🏭 Fully Automatic: 2,000–7,200+ tubes/hour
Inline automatic sealers integrated into the filling line run 40–120 tubes per minute. Required for mid-to-large cosmetic or pharmaceutical manufacturers producing above 20,000 tubes per shift. Investment range: $30,000–$120,000+. Sealed tube output per shift at 80 TPM and 85% OEE: approximately 32,640 tubes — the operating scale where ultrasonic sealing’s ROI compounds most rapidly.
⚠️ The Over-Specification Risk
Buying a 120 TPM inline sealer for a production line that genuinely needs 40 TPM wastes $40,000–$60,000 in capital that could fund a second production shift or a second tube format. The growth-buffer approach (size for 120% of current peak volume) is correct; over-specification beyond that is capital inefficiency dressed up as safety margin.
Production speed specifications should be verified with your actual tube material and fill viscosity — not lab-condition test tubes — before signing a purchase agreement.
Match Seal Quality Requirements to Your Product and Regulatory Context
The seal quality specification for a luxury skincare serum tube and the seal quality specification for a sterile pharmaceutical topical gel are not the same — and the machine features that deliver each are different. Getting this mapping right prevents both over-specification (paying for pharmaceutical-grade capability you don’t need) and under-specification (discovering your seal documentation doesn’t meet regulatory requirements during an audit).
| Product Category | Seal Quality Priority | Relevant Standard | Machine Feature Required |
|---|---|---|---|
| Pharmaceutical Topicals (Rx) | Hermeticity, sterility, tamper-evidence, documentation | FDA 21 CFR 211, EU GMP Annex 1, USP <671> | Per-cycle data logging, Cpk ≥1.33, closed-loop amplitude control, IQ/OQ/PQ package |
| OTC Pharmaceutical Tubes | Tamper-evidence, seal strength >30N, traceability | ISO 11607, FDA cGMP 21 CFR 211.132 | Electronic batch recording, password-protected parameters, automatic reject for out-of-spec seals |
| Premium Cosmetics | Visual consistency, clean geometry, zero print damage | ISO 22716 (Cosmetic GMP) | Precision tooling, surface-safe sonotrode contact design, seal-width tolerance ≤0.2mm |
| Standard Cosmetics / Personal Care | Leak-free closure, consistent appearance | Brand specification, retailer QA standards | Reliable cycle control, statistical process monitoring, simple recipe storage |
A key metric to request from any supplier is Cpk — the Process Capability Index, which measures how consistently a process stays within specification. A Cpk of 1.33 means the process produces no more than 63 defects per million opportunities — the standard minimum target for regulated pharmaceutical packaging. Conventional heat sealers on well-maintained equipment typically achieve Cpk 1.0–1.2. Ultrasonic sealing, correctly specified, consistently achieves Cpk 1.5–2.0.
That difference translates directly into audit readiness: a Cpk of 1.5 generates statistically defensible seal quality documentation. A Cpk of 1.0 means your process is producing defects at a rate that requires larger sample sizes to verify conformance — and that the process is running close to its tolerance boundary.
Evaluate Machine Integration and Compatibility with Your Existing Line
A sealing machine that performs perfectly as a standalone unit but cannot synchronize reliably with your upstream filling machine is a bottleneck dressed up as a solution. Integration is not a secondary consideration — it is as technically important as the sealing specification itself.
Communication Protocol
Confirm that the sealing machine’s PLC supports your filling line’s communication protocol. Modbus TCP, EtherCAT, and PROFINET are the most common in cosmetic and pharmaceutical production environments. Without protocol compatibility, the sealing machine cannot receive tube-present signals or line-speed synchronization from the filler — meaning timing mismatches generate jams and double-seal events.
Mechanical Infeed Compatibility
The sealing station must accept tubes at the pitch and orientation produced by your filling machine output conveyor. Confirm: tube infeed pitch (center-to-center distance between tube positions), tube orientation (neck up or neck down), and whether a transfer section is needed between filler discharge and sealer infeed. These details determine whether installation takes one day or two weeks.
Reject System Integration
Modern ultrasonic sealers with per-cycle quality monitoring can automatically reject tubes where seal energy, dwell time, or pressure deviated from specification. This requires an integrated reject mechanism — either a divert gate on the output conveyor or a push-reject arm — and confirmation that the reject event is logged against the batch record. Without this, out-of-spec seals pass to the finished goods stream.
Modular Scalability
Ask specifically: can this machine be upgraded from semi-automatic to fully automatic infeed without replacing the sealing core? Can a second sealing lane be added? Can vision inspection be integrated downstream? Modular design prevents the capital waste of replacing functional equipment to accommodate volume growth — and it is a meaningful signal that the supplier designed for your production lifecycle, not just your first purchase.
For a detailed view of how ultrasonic sealing integrates within a complete cosmetic tube production system — including filling, heading, and printing — the Miyoda Packaging Machinery tube filling and closing machine platform documents the integration architecture between filling, sealing, and downstream handling in a single production cell configuration.
See Ultrasonic Tube Sealing in Operation
Before finalizing any machine evaluation, watch a production-grade ultrasonic sealing line running on tube materials comparable to yours — not a laboratory demonstration on perfect test samples. The following video demonstrates an ultrasonic tube sealing machine operating on cosmetic and pharmaceutical tube formats:
When watching any sealing demonstration, observe the seal tail geometry across consecutive tubes, the cycle-to-cycle consistency, and how the machine handles tube transfer — these are the operational details that determine real-world performance.
Prioritize Reliability, Maintenance, and Service Support
The maintenance cost profile of ultrasonic sealing equipment is structurally different from thermal sealing equipment — and significantly more favorable. Understanding this before purchase prevents the common mistake of comparing purchase prices without accounting for the 5-year operating cost difference.
Here is what to evaluate and how to evaluate it:
- Sonotrode (Horn) Lifespan The sonotrode — the titanium or steel tool that contacts the tube tail — is the primary wear component in an ultrasonic sealing system. Service life runs 5–10 million cycles depending on material, amplitude setting, and usage intensity. On a line running 80 TPM at 85% OEE for two shifts daily, that translates to approximately 12–18 months before sonotrode inspection is warranted. Replacement cost: $300–$1,500 per sonotrode depending on specification. Request the cycle-count replacement threshold in writing before purchase.
- Converter (Transducer) Service Life The converter transforms electrical energy from the generator into mechanical vibration. Properly maintained converters reliably exceed 5 years of service on standard production schedules. They are not a routine consumable — but any supplier who cannot provide a converter service life estimate with reference to operating conditions is not prepared to support your equipment after installation.
- Generator Electronics The ultrasonic generator (the control unit that produces the high-frequency electrical signal driving the transducer) typically carries a 2-year warranty and a documented service life of 8–12 years. Ask for the generator’s protection features: overload shutdown, frequency auto-tuning (which compensates for sonotrode wear without manual recalibration), and diagnostic fault logging that identifies fault type before a service engineer visits.
- Annual Maintenance Cost Benchmarks Annual maintenance and spare parts costs for ultrasonic sealing equipment typically run 2–4% of equipment value — compared to 4–7% for conventional heat sealing equipment with more frequent heating element and jaw surface replacements. On a $40,000 machine investment, that difference is $800–$1,200 per year in additional maintenance budget savings, compounding over the equipment lifecycle.
- Remote Diagnostic Capability Confirm whether the generator includes remote diagnostic capability — the ability for the supplier’s technical team to connect to the machine’s control system over the internet to read fault logs, review process parameters, and guide corrective action without requiring an on-site visit. For international operations or facilities in locations where on-site service response takes 48–72 hours, remote diagnostics is the difference between a 30-minute fault resolution and a 3-day production stop.
- Spare Parts Availability Commitment Ask for lead times and stocking confirmation on the top 5 wear components: sonotrode, converter O-rings, pneumatic pressure regulator, sealing jaw guide bushings, and generator fuse/protection components. A supplier who cannot confirm stocking for all five items, with lead times in working days rather than “we’ll check,” is presenting a production risk that needs to be assessed before the purchase, not after.

A structured preventive maintenance schedule — sonotrode inspection, pressure verification, calibration — takes 2–4 hours per month and is the primary determinant of long-term machine reliability.
Demand Transparency and Validation Support from Every Supplier
The quality of a supplier’s validation documentation is the most reliable pre-purchase indicator of their post-purchase support quality. Suppliers who have genuine engineering depth in cosmetic and pharmaceutical tube sealing produce detailed, application-specific documentation because they have run the applications, solved the problems, and built the process knowledge into their records. Those who have not produce brochures.
Here is what to request — and what the response tells you:
| What to Request | Strong Supplier Response | Weak Supplier Response |
|---|---|---|
| Sample IQ/OQ protocol for pharmaceutical application | Provides sample document immediately; confirms whether included in price or quoted separately with specific cost | “We can support your validation process.” (No document provided) |
| Seal strength data for your tube material (ASTM F88 peel test) | Provides test data with stated conditions: tube material, wall thickness, amplitude setting, dwell time, ambient temperature | “Our seals are very strong — we have many satisfied customers.” |
| Cpk data from comparable production installations | Cites specific Cpk values (e.g., 1.67) from named production environments — or offers to share under NDA | “Our equipment consistently produces high-quality seals.” |
| Reference customer in your industry (cosmetic or pharma) | Provides name, facility location, contact for reference call within 48 hours | “We have many customers in your industry — references available upon request.” (Never materializes) |
| Factory acceptance test criteria for your tube specification | Proposes specific FAT criteria: throughput rate, seal strength threshold, Cpk target, visual quality standard — in writing | “We’ll test the machine before shipment, you can trust our QC process.” |
For pharmaceutical applications specifically, the IQ/OQ/PQ qualification framework for medical packaging equipment requires that validation protocols be written before testing begins — not reconstructed afterward from installation records. Any supplier who proposes to “help with documentation after installation” is inverting the sequence that regulators expect. The protocol must precede the installation event it is designed to qualify.
Ask the Right Questions Before You Compare Machines
Most machine comparisons fail because buyers compare specifications rather than applications. The right questions shift the conversation from “what can this machine do?” to “what will this machine do for my specific tube, material, volume, and compliance context?”
Use this checklist before your first serious supplier conversation:
- Have you run our tube material (specify: PE / PBL / ABL, diameter, wall thickness) on this specific machine? Ask for test data or a trial offer with our actual tube samples.
- What is the validated throughput at our target production speed with our tube material? Not rated speed — sustained throughput with documented cycle time at our fill product viscosity.
- What Cpk value does your sealing process achieve on comparable tube formats in production? Request documented Cpk values from existing installations, not lab-condition projections.
- What is the sonotrode replacement interval at our target production volume, and what is the cost per sonotrode? Calculate annual sonotrode cost as a line item in the TCO comparison.
- Can you provide a sample IQ/OQ validation protocol? For pharmaceutical buyers — confirm this is included in the machine price before signing.
- What are your top 5 wear component lead times and do you hold regional stock? Confirm stocking commitment for critical items in writing.
- What communication protocols does the machine support? Confirm compatibility with your filling line’s PLC before purchase.
- What is your on-site service response time commitment in our region? Ask for named contacts and contractual commitments — not assurances.
- Can we trial our actual tube samples at your facility before commitment? A supplier confident in their machine’s suitability for your application will say yes immediately.
- What is the modular upgrade path from current configuration to higher output? Confirm specific upgrade options and indicative costs — not just “it’s modular.”
Avoid Hidden Costs: Training, Changeover, and Downtime Risks
The purchase price and the annual maintenance estimate cover two of the five major cost categories in a sealing machine’s total cost of ownership. The three that are most consistently underestimated at the purchase stage are operator training, format changeover time, and unplanned downtime risk.
👩🏭 Operator Training Cost
Operator training for a semi-automatic ultrasonic sealer typically requires 1–2 days of supervised operation to reach proficiency. Fully automatic inline configurations take 2–4 days, covering fault recovery, maintenance tasks, and recipe management alongside the sealing operation itself. Request that the supplier include documented training materials — not just verbal instruction — so that operator turnover (an inevitable reality in production environments) can be managed with internal training resources rather than requiring a supplier return visit each time.
🔄 Format Changeover Time
Switching between tube formats — from a 22mm pharmaceutical tube to a 40mm cosmetic tube — requires sonotrode tooling change and parameter recipe recall. With quick-change tooling and HMI recipe storage, this takes 10–20 minutes. Without it, parameter re-entry and manual fixture adjustment can take 60–90 minutes. On a line running 5 different SKUs per week, the difference between a 15-minute and a 75-minute changeover represents 5 additional production hours recovered weekly — roughly 8–10% more usable production capacity per week without a single machinery upgrade.
⏰ Unplanned Downtime Risk
On a line producing 5,000 tubes per hour at a $0.15 contribution margin, each unplanned downtime hour costs $750 in lost output. If the nearest service engineer is 48 hours away and the machine doesn’t have remote diagnostic capability, a fault that a technician could resolve in 20 minutes becomes a 48-hour production stop worth $36,000 in lost margin. This is not a hypothetical — it is the operating reality for international buyers sourcing equipment from suppliers without genuine regional service presence. Verify service coverage geography before purchase, not after installation.
📐 Calibration and Recalibration
Ultrasonic sealing systems require periodic amplitude calibration — verification that the sonotrode is delivering the commanded energy level. Well-maintained systems with automatic frequency tuning compensate for minor sonotrode wear without manual recalibration. Machines without auto-tuning require manual calibration checks every 3–6 months. Confirm which type the machine uses, and request a calibration procedure document so your maintenance team can perform routine calibration in-house without requiring a supplier service visit.
Make the Confident Choice: Partner with a Supplier Who Understands Your Industry
The machine you buy and the supplier you choose are not separable decisions. The engineering support, application knowledge, and service responsiveness that determine your production performance over the next 10 years come from the supplier relationship — not from the machine specification sheet.
Here is what distinguishes a genuine industry-specialist supplier from a general equipment vendor in the context of cosmetic and pharmaceutical tube sealing:
- Application-Specific Experience A genuine specialist can tell you immediately which amplitude setting range works for your tube material at your target wall thickness, which sonotrode geometry produces the best seal geometry on your tube diameter, and which parameters require adjustment when switching between PE and ABL formats. This knowledge comes from having run hundreds of qualification trials across real production environments — not from reading the same technical brochures you have access to.
- Compliance Documentation Capability For pharmaceutical buyers: a supplier who routinely supports pharmaceutical clients has IQ/OQ protocols, FDA 21 CFR Part 11-compatible data logging, and audit-trail documentation as standard product features — because their clients demand them. A supplier who does not have this documentation ready-to-show has not been asked for it before, which tells you something specific about their pharmaceutical client base.
- Transparent TCO Presentation A supplier confident in their equipment’s total cost of ownership will help you build the 5-year TCO comparison — including their machine against competitors — because the analysis favors quality equipment over the purchase-price-only comparison. A supplier who resists TCO analysis or provides only headline purchase prices is either not confident in their equipment’s operating economics or is assuming you won’t run the numbers.
- Distributor and Agent Support Infrastructure For distributors and agents representing sealing equipment: the supplier who provides co-branded technical documentation, pre-sales sample testing capability, regional spare parts stocking, and dedicated technical training for your sales engineers is treating you as a long-term channel partner. The supplier who provides a price list and a brochure PDF is treating you as a transaction. The difference determines whether you can confidently represent the equipment to your pharmaceutical and cosmetic clients — or whether you’re selling from a spec sheet and hoping the installation works out.
At Miyoda Packaging Machinery, the tube sealing and filling machine range is designed specifically for cosmetic and pharmaceutical tube manufacturers — with application-specific configuration, production trial support using customer tube samples, and full technical documentation for both direct buyers and the distributors and agents who represent the equipment in their markets. The ultrasonic tube sealing guide for cosmetic and pharmaceutical manufacturers documents the specific machine configurations, material compatibility data, and ROI analysis relevant to this purchase decision.
A specialist supplier runs your actual tube samples before the purchase, not a generic demonstration on their standard test material. That distinction is what makes a trial meaningful.
Ready to Evaluate Ultrasonic Sealing for Your Specific Production?
Send us your tube samples and production parameters — we’ll run a compatibility trial and deliver a detailed report covering seal strength, cycle time, process Cpk, and projected ROI timeline for your production volume. No generic demo. Your tubes, your data.
View Sealing Machine Specifications Read More Technical Guides
Frequently Asked Questions
Answers to the questions cosmetic and pharmaceutical tube manufacturers — and the distributors and agents who represent packaging machinery — ask most often when evaluating ultrasonic tube sealing equipment.
1. How does ultrasonic sealing compare to heat sealing for laminated tubes?
Ultrasonic sealing generates heat at the molecular interface between tube wall layers through internal friction — not by conducting heat inward from a heated jaw surface. For laminated tubes, this is the critical difference: heat sealing risks thermal degradation of the outer print layer and, on ABL tubes, delamination of the aluminum-polymer bond. Ultrasonic sealing delivers stronger, more consistent seals without these risks. Published Cpk comparisons show ultrasonic sealing achieving 1.5–2.0 versus 1.0–1.2 for well-maintained heat sealers on the same tube formats — the difference between audit-ready process documentation and marginal conformance.
2. Can one machine handle multiple tube materials and diameters?
Yes — but only with the correct tooling and parameter configuration for each format. A modern ultrasonic sealer with adjustable amplitude, programmable dwell time, and recipe storage can cover tube diameters from 16mm to 60mm and materials from single-layer PE through multi-layer ABL, using interchangeable sonotrode tooling. The key is confirming with the supplier that each of your specific tube formats has been tested on this machine and that a qualified parameter recipe exists for each one. “It can handle multiple materials” without documented parameter data for your specific tubes is marketing language, not a qualified claim.
3. What seal strength should I expect for pharmaceutical-grade tubes?
For pharmaceutical tube applications, the target seal strength is typically above 30 N per 15mm width, measured per ASTM F88 peel strength testing. Ultrasonic sealing on standard pharmaceutical laminate tubes consistently achieves 30–50 N per 15mm with Cpk values above 1.33 — the minimum process capability target for regulated packaging. Request test data from the supplier using your specific tube material, not their standard test samples, before purchase.
4. How do I ensure hermetic sealing for sterile products?
Hermetic sealing for sterile pharmaceutical applications requires three machine features working together: real-time amplitude control (confirming the sonotrode is delivering the commanded energy level each cycle), per-cycle process data logging (recording actual amplitude, dwell time, and pressure for batch record documentation), and automatic rejection of any tube where seal parameters deviated from specification. Combine this with appropriate in-line leak testing — pressure decay or vacuum decay systems — to provide 100% seal integrity verification before tubes enter the finished goods stream.
5. Is ultrasonic sealing suitable for aluminum-plastic composite (ABL) tubes?
Yes — and for ABL tubes specifically, ultrasonic sealing is the preferred method over conventional heat sealing. The aluminum foil layer in ABL acts as a heat reflector on conventional heat sealers, creating uneven thermal distribution that risks delaminating the aluminum-polymer bond. Ultrasonic sealing bonds the polymer layers on either side of the aluminum without generating the thermal gradient that causes delamination. Confirm with the supplier that the machine has been validated on your specific ABL construction (foil thickness, laminate layer sequence) — performance varies by ABL specification.
6. What maintenance is required for ultrasonic sealing systems?
Routine maintenance for an ultrasonic sealing system covers four levels: daily (clean sonotrode contact surface; inspect for product residue or wear marks), weekly (check pneumatic pressure settings; run a seal quality verification on 5 sample tubes), monthly (full amplitude calibration verification; inspect converter connections; measure sonotrode wear against replacement threshold), and annually (full electrical diagnostic on generator; sonotrode replacement if cycle count has reached the replacement threshold). Annual parts and maintenance cost typically runs 2–4% of machine value — materially lower than equivalent hot-jaw sealing equipment.
7. Can I integrate an ultrasonic sealer into my existing tube filling line?
Most modern ultrasonic sealers are designed for inline integration with standard tube filling machines via standardized industrial communication protocols (Modbus TCP, EtherCAT, or PROFINET). Before purchase, confirm: protocol compatibility with your filling machine’s PLC, tube infeed pitch and orientation requirements, mechanical interface dimensions, and whether a transfer section is needed between filler discharge and sealer infeed. Request the machine’s electrical interface drawing and I/O list — if the supplier cannot provide these documents, the integration specification is insufficiently defined for a capital purchase commitment.
8. How long does changeover take between different tube sizes?
With quick-change sonotrode tooling and HMI recipe storage, format changeover between significantly different tube diameters takes 10–20 minutes. Without these features, manual fixture adjustment and parameter re-entry adds 40–70 minutes. For a facility running 5 SKU changes per week, the difference between 15-minute and 75-minute changeovers recovers 5 production hours weekly — roughly 8–10% additional production capacity without any machine upgrade. Quick-change tooling and recipe storage are not optional features for multi-SKU production environments; they are the primary cost-reduction drivers beyond the sealing quality improvement.
9. Do operators need special training for ultrasonic sealing machines?
Operators need to understand three areas specific to ultrasonic sealing: amplitude settings (and what changes in amplitude affect), horn alignment verification (sonotrode must contact the tube tail evenly across its full width — misalignment causes asymmetric seals), and fault diagnostics (how to interpret the machine’s alarm messages and what the corrective action is for each). Most operators reach operational proficiency in 1–2 days on a semi-automatic sealer and 2–4 days on a fully automatic inline configuration. Request that the supplier provide written training materials with your machine — not just verbal instruction — so internal training can cover operator turnover without requiring supplier involvement.
10. What happens when a seal fails during production?
Advanced ultrasonic sealing systems with per-cycle quality monitoring detect seal failures in real time by measuring actual sonotrode energy delivery against the target window. When a cycle falls outside specification — due to material variation, sonotrode misalignment, or parameter drift — the machine triggers an automatic rejection at the output conveyor, logs the event against the batch record, and alerts the operator. This prevents out-of-spec seals from reaching the finished goods stream. Machines without this capability rely on statistical end-of-line inspection, which will always allow some failures through statistically. For pharmaceutical applications, 100% seal integrity verification is the expected standard.
11. Are spare parts readily available, especially for the ultrasonic stack?
Spare part availability depends entirely on the supplier’s regional logistics infrastructure. The critical question is not whether parts are available — it is what the lead time is for the sonotrode (the most likely production-stopping wear component). Ask specifically: “What is your lead time for sonotrode replacement, and do you hold regional stock?” A lead time of more than 5 working days without confirmed local stock represents a meaningful production risk that should be either mitigated with an on-site spare sonotrode or weighted in the supplier comparison. The tube packaging machine buyer’s guide for pharmaceutical and cosmetic manufacturers covers spare parts evaluation methodology in detail for both sealing and filling equipment.
12. Can the machine handle printed or decorated tubes without damaging the surface?
Yes — provided the sonotrode contact face is specifically designed to avoid contact with the printed tube body. In a correctly specified ultrasonic sealing fixture, the sonotrode contacts only the tube tail (the sealed end, which is unprinted) and the jaw contact areas are lined with non-marking materials. However, if tube body geometry places printed areas within 3–5mm of the seal zone, confirm with the supplier that the sonotrode design accommodates this without surface contact. Ask to see photographs of sealed tubes from your specific tube format — surface marking caused by sonotrode contact shows as a characteristic pressure mark pattern that is immediately visible.
13. How do I validate the sealing process for regulatory audits?
Sealing process validation for pharmaceutical regulatory audits follows the IQ/OQ/PQ framework. The machine supplier provides the IQ protocol (installation verification checklist), the OQ protocol (operational parameter verification test procedures), and the PQ protocol (production-condition performance testing). Your quality team executes these protocols during commissioning and generates the completed validation package — the documented evidence that the sealing process operates within specified parameters. Modern ultrasonic systems with per-cycle data logging, password-protected parameter settings, and electronic audit trail capability are specifically designed to generate the data these protocols require. Confirm that the machine’s data logging is configurable to meet FDA 21 CFR Part 11 requirements for electronic records and signatures before purchase.
14. What is the typical lifespan of an ultrasonic sealing horn?
Sonotrode service life ranges from 5 to 10 million sealing cycles, depending on tube material (ABL requires slightly higher amplitude than PE, accelerating wear marginally), amplitude setting (running above the minimum effective amplitude for a given material accelerates wear without improving seal quality), and sonotrode material (titanium alloy sonotrodes outlast aluminum alloy by approximately 2× for high-volume production). On a line running 80 tubes per minute at 85% OEE for two 8-hour shifts daily, 5 million cycles is reached in approximately 10–12 months. Budget for sonotrode replacement as an annual line item in your maintenance cost plan.
15. Is there any risk of overheating sensitive cosmetic or pharmaceutical formulations?
No — this is one of the primary technical advantages of ultrasonic sealing over thermal methods. The heat generated by ultrasonic friction is confined to the molecular interface of the tube tail material and does not conduct into the fill product column above the seal zone. Independent stability testing on standard 35–50mm diameter cosmetic tubes shows no measurable temperature increase in the product zone during properly executed ultrasonic sealing cycles. For heat-sensitive pharmaceutical actives — retinoids, certain antibiotics, biologic-derived compounds — this is not a marginal advantage; it is a formulation protection requirement that heat sealing cannot reliably satisfy.
16. Can the system be upgraded for higher output in the future?
On modular platform designs, yes — specifically, semi-automatic configurations can be upgraded to automatic infeed without replacing the sealing core, additional sealing lanes can be added to increase throughput, and vision inspection systems can be integrated downstream of the sealing station. Confirm the modular upgrade path and indicative costs before purchase — a supplier who provides this information upfront is designing for your production lifecycle; one who cannot provide it is not. The upgrade path should be documented in the purchase agreement as available options, not promised informally.
17. How do I troubleshoot weak or inconsistent seals in production?
The four most common root causes of weak or inconsistent ultrasonic seals, in order of frequency: (1) sonotrode misalignment — the sonotrode contact face is not parallel to the anvil, producing uneven pressure across the seal width; (2) worn sonotrode — amplitude delivery drops as the sonotrode approaches its replacement threshold; (3) incorrect amplitude setting for the current tube material or batch — wall thickness variation between tube batches sometimes requires parameter adjustment; (4) product contamination in the seal zone — fill product deposited in the tube tail by an over-filling nozzle creates a barrier between the plastic layers that prevents complete fusion. Modern diagnostic tools on current-generation machines identify which of these causes is active by analyzing the sonotrode energy delivery pattern during the faulty cycles — a supplier with good remote diagnostic capability can often identify the root cause from logged data without an on-site visit.
18. Is ultrasonic sealing more environmentally sustainable than thermal methods?
Across three sustainability dimensions, yes. Energy consumption: ultrasonic sealers draw power only during the active weld cycle (typically 0.5–2 seconds per tube), while heated-jaw systems maintain continuous power draw to keep jaws at operating temperature. Comparative analysis from Herrmann Ultrasonics documents 30–50% energy reduction per seal compared to equivalent thermal processes. Consumables: ultrasonic sealing uses no sealing tapes, adhesives, or hot wires — eliminating both the purchase cost and the disposal cost of those consumables. Emissions: no burnt adhesive or thermal degradation products, which reduces fume extraction requirements and improves the working environment.
19. What certifications should the machine meet for pharmaceutical and cosmetic use?
For pharmaceutical applications: CE marking (EU machinery directive compliance), GMP-compatible contact surface materials (316L stainless steel or documented equivalent), ISO 13849 functional safety compliance for machine guarding, and the ability to support IQ/OQ/PQ documentation. For FDA-regulated US market production: 21 CFR Part 11-compatible data logging for electronic batch records. For cosmetic applications: CE marking and ISO 22716 (Cosmetics GMP) compatible design — primarily meaning cleanable surfaces, no dead zones, and material traceability. Request the Declaration of Conformity document for all applicable directives — this is the legally binding statement of compliance, not the product specification sheet.
20. Can I test my tubes on the machine before purchasing?
Any supplier with genuine confidence in their machine’s suitability for your application will provide tube sample testing as a standard pre-purchase service — not as a paid evaluation or a favor. The trial should run your actual tube samples (not the supplier’s standard test tubes), under documented parameter settings, with output data including seal strength measurement, cycle time, and visual quality assessment provided to you in a written report. This report is also your first piece of machine qualification evidence — it documents the parameter settings that produced compliant seals on your tube material, which is the starting point for your production recipe. If a supplier charges for pre-purchase sample testing or declines to provide it, that should be weighted heavily in your evaluation.
Start Your Evaluation with Real Production Data — Not a Brochure
The Miyoda Packaging Machinery ultrasonic sealing platform is configured for your specific tube material, diameter, and compliance context — not shipped from a standard catalog. Share your tube samples and production parameters, and our engineering team will return seal strength data, cycle time confirmation, and a projected ROI timeline for your production volume.
View Full Machine Specifications Compare All Tube Sealer Types















