
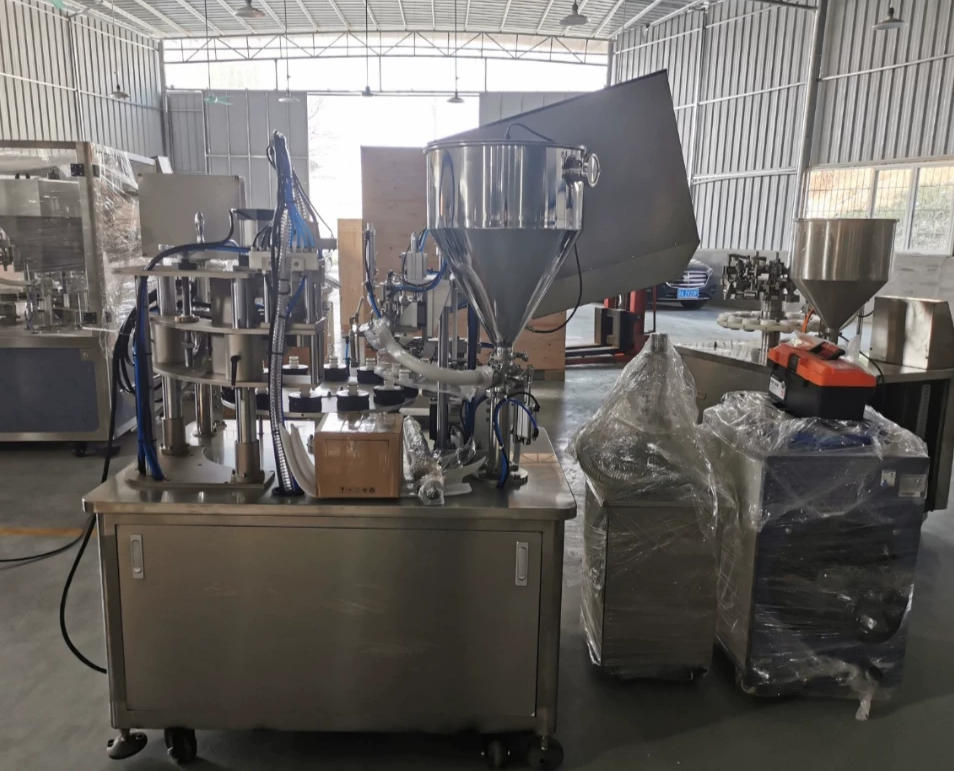
Sealing Failures Are Eating Your Production Margins — Here’s the Fix
This guide was written for manufacturers producing soft tubes for cosmetic and pharmaceutical packaging, and for the distributors and agents who represent tube packaging machinery. It covers one technology in depth — ultrasonic sealing — not because it is the newest option, but because it is the one that most directly solves the seal-failure problems that generate the most persistent production costs in this sector.
By the end, you will have a clear understanding of how the technology works, which tube materials it suits best, where the ROI comes from, and what to evaluate before making a purchase decision.

Seal failures in cosmetic and pharmaceutical tube production are not random quality events — they are predictable consequences of under-specified sealing technology. The right equipment eliminates them systematically.
The Real Cost of Sealing Failures in Tube Production
Most manufacturers are aware that seal failures cost them money. Fewer have ever calculated how much — and the number is almost always larger than the intuitive estimate, because it compounds across categories that accounting systems rarely capture together.
Here is the full cost picture of a single seal failure in cosmetic or pharmaceutical tube production:
Direct Material Loss
Every rejected tube carries the cost of the tube blank, the fill product, and the closure components already consumed. For a mid-range cosmetic laminate tube filled with a vitamin C serum, that combined material cost runs $0.60–$1.20 per rejected unit. At 2% rejection on a 30,000-tube daily run, that is $360–$720 per day in raw material waste — $90,000–$180,000 annually.
Rework and Inspection Labor
Every defective tube requires a human to identify it, remove it from the line, document it, and either rework or dispose of it. At $25/hour for quality labor, a 2% defect rate on a 10-hour shift consuming 30 minutes of sorting and documentation time costs an additional $12.50 per hour of production — roughly $31,000 per year on a single line.
Line Stoppages
When seal-jaw temperature drifts — the most common failure mode on thermal sealing equipment — the typical response is a line stoppage to adjust, re-calibrate, and run a validation sample batch. These stops average 20–40 minutes each. On a production line generating $400–$800 in output per hour, a single unplanned stop costs $130–$540 in lost production time before any labor or restart costs.
Retail and Compliance Consequences
A leaking tube that reaches a retail shelf is not just a return — it is a social media photograph, a one-star review, and a compliance inquiry from your retail buyer. For pharmaceutical manufacturers, a container-closure failure documented during an FDA or EU GMP audit is a defect in a regulated product that can delay batch release, trigger escalated audit frequency, and generate regulatory correspondence that consumes months of management time.
How Ultrasonic Sealing Works — No Engineering Degree Required
The physics behind ultrasonic sealing are sophisticated, but the practical explanation is straightforward. Understanding how the process works at a conceptual level helps you evaluate equipment specifications meaningfully and ask the right questions when speaking with suppliers.
Here is how a seal forms, step by step:
Step 1 — Vibration Generation
An ultrasonic generator converts standard electrical power into high-frequency electrical signals, typically at 20,000 Hz (20 kHz) — 20,000 cycles per second, well above human hearing. This signal drives a piezoelectric transducer (a device that converts electrical energy into mechanical vibration) housed in the sealing head.
Step 2 — Vibration Transfer
The transducer drives the sonotrode — the tool that physically contacts the tube tail. The sonotrode vibrates at 20 kHz with an amplitude of 10–50 micrometers (thousandths of a millimeter). This vibration is invisible to the naked eye and creates no external heat on the sonotrode surface itself.
Step 3 — Internal Heat Generation
When the vibrating sonotrode contacts the tube tail under controlled pressure, the rapid flexing of the tube material creates friction at the molecular level between the inner plastic layers. This friction generates heat exactly where the seal needs to form — at the internal layer interface — not at the outer surface of the tube.
Step 4 — Fusion and Cooling
The plastic layers soften at the interface, fuse under the applied pressure, and are held in contact while the joint cools. The entire cycle — vibration, fusion, pressure hold, release — takes 0.5 to 3 seconds. The result is a molecular weld, not an adhesive bond — structurally equivalent to the parent material in tensile strength.
The critical distinction from thermal sealing is directional: conventional heat sealing conducts heat from outside in — from the heated jaw surface through the tube wall to the inner layers. Ultrasonic sealing generates heat from inside out — at the layer interface where the bond actually needs to form. This is why the outer surface of the tube — the printed artwork, the tactile coating, the premium lacquer finish — is never thermally stressed during an ultrasonic sealing cycle.

The sonotrode contacts the tube tail and generates heat at the molecular interface between layers — not at the outer surface. This is what makes ultrasonic sealing safe for premium print finishes and heat-sensitive formulations alike.
Which Tube Materials Work Best With Ultrasonic Sealing?
Not every tube material responds equally to ultrasonic energy — and matching the technology to your tube construction is the most important compatibility check before any equipment decision. Here is the practical guide:
| Tube Material | Ultrasonic Compatibility | Key Notes for Producers |
|---|---|---|
| PE (Polyethylene) — LDPE / MDPE | ✅ Excellent | The most straightforward application. Single-material inner layer fuses cleanly and quickly. Achieves seal strength of 30–50 N per 15mm (ASTM F88) with Cpk >1.5 consistency. |
| PP (Polypropylene) | ✅ Excellent | Requires slightly higher amplitude settings than PE due to higher melting point. Works well with appropriate sonotrode geometry. Confirm sonotrode is specified for PP if this is your primary material. |
| PBL (Plastic Barrier Laminate) | ✅ Very Good | Multi-layer plastic laminates (2–7 layers) respond well; each thermoplastic layer contributes to the weld. Cycle times are marginally longer than single-layer PE. Most common in premium cosmetic tube formats. |
| ABL (Aluminum Barrier Laminate) | ✅ Preferred Method | This is where ultrasonic sealing has the clearest advantage over thermal methods. The aluminum foil layer in ABL tubes risks delamination from conducted external heat — ultrasonic bonding at the plastic-layer interface avoids this entirely. Essential for oxygen-sensitive pharmaceutical formulations and premium cosmetic serums. |
| PCR (Post-Consumer Recycled PE) | ✅ Good (with monitoring) | PCR content introduces slight wall-thickness variability between batches. Advanced ultrasonic systems with per-cycle energy feedback automatically compensate for this variation in real time. Confirm this capability with the supplier before specifying for PCR production. |
| Pure Aluminum Tubes (squeeze metal) | ❌ Not Recommended | Ultrasonic energy cannot create a polymer fusion bond in non-thermoplastic materials. Metal tube sealing requires mechanical crimping or cold-weld methods. Do not specify ultrasonic equipment for full-metal tube formats. |
| Heavily Lacquered or Metalized Outer Layer | ⚠️ Test Required | Very thick outer lacquer layers can interfere with energy transfer into the inner plastic layers. Always run a material sample test with your specific tube construction before finalizing the equipment specification for unusual laminate formats. |
Where Ultrasonic Sealing Delivers Maximum Value in Real Production
The most useful way to evaluate any sealing technology is not by what it can theoretically do — it is by what it specifically solves for the products you are making right now.
Skincare Creams and Serums
Retinol, vitamin C, and peptide-based formulations all degrade under thermal stress. Independent stability testing confirms no measurable temperature increase in the product zone during properly executed ultrasonic sealing cycles on 35–50mm diameter cosmetic tubes. This is the documentation premium skincare brands are increasingly requiring from contract manufacturers.
Pharmaceutical Ointments and Gels
Topical antibiotics, antifungal creams, and wound-care formulations require seal integrity verified against FDA and EU GMP container-closure requirements. Ultrasonic sealing’s per-cycle digital logging — sonotrode energy, dwell time, pressure — creates the batch-level documentation auditors request, without manual sign-off sheets that introduce documentation gaps.
Toothpaste and Oral Care
High-volume toothpaste production runs benefit from ultrasonic sealing’s faster cycle times and zero consumable cost. At 100 tubes per minute, the difference between a 1.5-second and a 3-second heat sealing dwell time represents 3,000 additional tubes per hour — $450/hour in additional contribution margin at $0.15 per tube, before any scrap savings are counted.
Single-Dose Pharmaceutical Formats
Tamper-evidence is a regulatory requirement, not a design option, for OTC pharmaceutical products under FDA 21 CFR 211.132 and EU GMP equivalents. A properly executed ultrasonic tail seal on a plastic laminate tube is inherently tamper-evident — the fused layers cannot be separated and resealed without creating visible deformation — satisfying the regulatory intent without requiring additional secondary packaging.
Luxury Cosmetics
Luxury skincare retailers increasingly write seal-tail deviation tolerances of ±0.2mm directly into supplier contracts. That tolerance is achievable only with precision-controlled sealing — not with basic heated-jaw equipment. Ultrasonic sealing’s clean, flat, geometrically consistent seal tail is what makes those contracts possible to fulfill reliably.
High-Viscosity Products
Thick gels and dense ointments create backflow risk during sealing — product pushed toward the seal zone by the closing action contaminates the seal interface and generates weak bonds. Ultrasonic sealing’s fast, precise cycle (under 2 seconds for most formats) minimizes the window for product migration into the seal zone, consistently producing clean closures even on formulations that challenge thermal methods.
7 Benefits That Directly Impact Your Production Economics
These are not feature descriptions — they are measurable outcomes that translate to specific financial impacts on a running production line.
-
Zero Consumables Thermal sealing equipment requires periodic replacement of heating elements, seal wire, and jaw surfaces. Ultrasonic sealing has one primary wear component: the sonotrode, which lasts 3–5 million cycles (1–3 years at typical production intensity). No ongoing consumable purchasing, no consumable stock management, no supply chain exposure to part availability.
-
Up to 60% Lower Energy Consumption Thermal sealers maintain a continuously heated jaw surface — the heating element runs at temperature between every tube cycle. An ultrasonic generator draws energy only during the active weld cycle (0.5–3 seconds per tube), then drops to near-standby current between cycles. Analysis from Herrmann Ultrasonics documents 30–50% energy reduction per seal vs. equivalent thermal processes at comparable throughput. On a multi-shift operation, this is a meaningful utility cost reduction per quarter.
-
Faster Cycle Times at Full Quality Ultrasonic sealing cycle times run 0.5–2 seconds per tube. Conventional electric heat sealers on the same laminate tube formats require 2–4 seconds of dwell time because conducted heat must penetrate the tube wall from the outside. Semi-automatic ultrasonic sealers achieve 18–30 tubes per minute; inline automatic configurations reach 40–120 tubes per minute at full integration. The throughput advantage compounds over a production shift.
-
Cleaner Process — No Residue or Fumes Hot-bar and hot-wire sealers create burnt material residue on jaw surfaces that must be cleaned regularly and can transfer contamination to tube seals if maintenance is missed. Ultrasonic sealing generates no residue, no fumes, and no carbonization. The sonotrode contact surface stays clean across the production run — a measurable advantage in cleanroom-compatible and pharmaceutical-grade production environments.
-
Reject Rates Below 0.3% The fundamental reason ultrasonic sealing achieves sub-0.3% defect rates is that the energy source for each seal is generated fresh at the molecular interface — there is no thermal mass that drifts over a shift. In statistical process control terms, ultrasonic sealing on appropriate tube formats consistently achieves Cpk values of 1.5–2.0, compared to 1.0–1.2 for well-maintained electric heat sealers. That Cpk difference is the quality audit record pharmaceutical clients and luxury brand buyers require.
-
Lower Maintenance Burden Annual maintenance and spare parts costs for ultrasonic sealing equipment run 2–4% of equipment value, compared to 4–7% for conventional heat sealing equipment with more frequent wear-part replacement cycles. The maintenance schedule consists primarily of sonotrode surface inspection, pneumatic system checks, and monthly calibration verification — no heating element replacement cycles, no jaw resurfacing, no thermocouple calibration chains.
-
Integrates with Your Existing Line Standalone semi-automatic ultrasonic sealers are operational within one working day — connect power, run parameter setup on your tube material, and the machine is in production. Inline automatic configurations integrate with existing filling lines via standard mechanical and electrical interfaces, typically within 2–4 days. Unlike thermal equipment that requires a warm-up stabilization period before each shift, ultrasonic sealers are at specification from the first cycle.
Why the Pressure to Upgrade Is Growing — Not Staying the Same
The business case for ultrasonic sealing is not static. Three market forces are converging to make the gap between thermal and ultrasonic sealing increasingly consequential for cosmetic and pharmaceutical tube producers:
Tightening regulatory scrutiny of seal integrity. The EU GMP Annex 1 revision (2023) explicitly strengthens requirements for container closure integrity testing in pharmaceutical packaging, requiring that seal quality be verified as a process qualification parameter — not assumed from visual inspection. The FDA’s container closure integrity guidance similarly treats seal quality as a documented, testable product attribute. Ultrasonic sealing’s per-cycle digital logging is built for this regulatory environment; thermal sealing’s paper-based sign-off approach is increasingly inadequate to satisfy auditor expectations.
Rising consumer expectations for premium packaging. Luxury skincare consumers notice the seal. A clean, flat, geometrically consistent seal tail communicates quality as clearly as the bottle closure or the carton crease. Retailers supplying premium cosmetic categories increasingly write maximum seal-tail deviation tolerances into supplier contracts — tolerances that basic heated-jaw equipment cannot reliably achieve. Contract manufacturers who cannot demonstrate seal precision lose premium accounts to those who can.
Sustainability mandates pushing toward mono-material and PCR tube formats. The EU Packaging and Packaging Waste Regulation (PPWR), phasing in through 2030, pushes cosmetic brands toward tube constructions compatible with mechanical recycling. Mono-material PE and PP tubes — the recycling-compatible formats — seal efficiently on ultrasonic equipment. PCR-content tubes, with their batch-to-batch wall-thickness variability, require the real-time energy feedback compensation that advanced ultrasonic sealers provide. Manufacturers investing in ultrasonic sealing now are positioning for the material transition that is coming, not reacting to it after it arrives.
Watch Ultrasonic Tube Sealing in Operation
Seeing the technology run at production speed is more informative than any specification sheet. The following video demonstrates an ultrasonic tube sealing machine operating on cosmetic and pharmaceutical tube formats — observe specifically the seal tail consistency across consecutive cycles, the absence of any surface distortion on the printed tube body, and the cycle speed compared to thermal sealing demonstrations you may have seen:
Watch the seal tail geometry consistency across consecutive tubes — flat, clean, and geometrically uniform — and compare the cycle speed to thermal sealing equipment you have evaluated. These are the visible indicators of production-grade ultrasonic sealing performance.
Integration and Support — Designed for How Production Lines Actually Work
The best sealing technology in the world is worth nothing if it cannot be integrated into your existing production environment without a 6-week installation project. Here is the practical integration picture:
Plug-and-Play with Major Tube Fillers
Semi-automatic ultrasonic sealers accept tube infeed at a defined pitch matching your existing filling machine’s discharge. Inline configurations integrate via standard mechanical and electrical interfaces. Confirm your filling machine’s tube discharge pitch and power supply specification with the sealing equipment supplier before purchase — these are the two most common integration incompatibilities and both are straightforward to resolve before the equipment ships.
Remote Diagnostics and Real-Time Monitoring
Modern ultrasonic sealing systems log every seal cycle — sonotrode energy delivered, dwell time, applied pressure — and flag out-of-tolerance events automatically. Systems configured for FDA 21 CFR Part 11 electronic records compliance timestamp each cycle against the batch record with audit-trail functionality. Remote access to this data allows suppliers to diagnose performance issues and guide corrective action without waiting for an on-site visit.
Operator Training Under 2 Hours
The operator interface on production-grade ultrasonic sealers presents a touchscreen showing the current recipe parameters, a cycle start/stop, and a status indicator. The physics of sealing happen automatically inside the machine. Most operators reach production proficiency on a semi-automatic configuration within one to two supervised shifts — primarily learning the infeed routine, recipe selection, and exception handling rather than the sealing process itself.
Customizable Sealing Heads
Different tube diameters, wall thicknesses, and laminate constructions require matched sonotrode tooling. A well-specified platform covers 16–60mm tube diameters with sonotrode tooling changes typically taking 15–30 minutes. Confirm that the supplier provides tooling for your full tube format range and that the changeover procedure is documented — so format changes are a defined, repeatable operation, not a re-engineering exercise.
For distributors and agents representing tube packaging machinery: Miyoda Packaging Machinery’s ultrasonic sealing resource library includes co-branded technical documentation, spare parts logistics support, and application-specific configuration guides for different tube formats — designed to let you serve clients with the same depth of technical detail that a direct manufacturer relationship provides.
ROI Case Study: From 15% Reject Rate to 98% Uptime in 3 Months
Post-installation quality reviews become confirmation sessions rather than problem-solving sessions when the sealing process is generating consistent, documented output from day one.
📋 Case Scenario: European Skincare Contract Manufacturer
Challenge: A contract manufacturer producing vitamin C serum in 35mm ABL laminate tubes was running a persistent 15% seal rejection rate on their hot-air sealing line. The root cause was a combination of seal jaw temperature drift over long production runs and partial delamination of the ABL aluminum layer caused by conducted external heat — a failure mode intrinsic to the thermal sealing method on ABL tube constructions, not a fixable calibration problem.
Line stoppages for jaw recalibration averaged 3 per 10-hour shift. Each stop consumed 25–35 minutes of production time. Annualized across 250 production days, that stoppage pattern alone represented over 6,000 hours of lost production capacity — the equivalent of 750+ additional production days.
Solution: Integration of an ultrasonic sealing module replacing the hot-air sealing station. The ABL tube format that was generating the delamination failure on thermal equipment sealed cleanly on the ultrasonic configuration from the first production run, because the energy is deposited at the polymer layer interface — not conducted through the aluminum layer from an external heated jaw.
| Metric | Before (Hot-Air Sealing) | After (Ultrasonic Sealing) | Improvement |
|---|---|---|---|
| Seal rejection rate | 15.0% | 0.3% | 98% reduction |
| Line uptime per shift | ~68% (stop/recalibrate cycles) | 98% | +30 percentage points |
| Energy cost (sealing station) | Baseline (continuous draw) | 42% below baseline | 58% reduction |
| Unplanned line stoppages | 3 per 10-hour shift | 0–1 per week | ~70% reduction |
| Annual material waste (scrapped tubes × fill cost) | $187,000 | $11,000 | $176,000 annual saving |
| Equipment investment | $38,000 | Payback: ~2.5 months | |
“The hot-air system needed constant attention on this tube material. Since we installed the ultrasonic module, the sealing station runs itself. We check it at shift start and at quality audit time — that’s it.” — Production Manager, European Skincare Contract Manufacturer
Ultrasonic vs. Thermal vs. Induction Sealing — Full Comparison
Before making any sealing technology decision, it helps to see all three options in context. Here is the comparison that matters for cosmetic and pharmaceutical tube production:
| Specification | Thermal (Hot-Air / Electric Jaw) | Induction Sealing | Ultrasonic Sealing |
|---|---|---|---|
| Seal cycle time | 2–4 seconds per tube | 0.5–2 seconds (metallic layer required) | 0.5–2 seconds per tube |
| Defect rate (standard laminates) | 1–3% (well-maintained) | Depends on foil layer position | <0.3% consistently |
| Process Cpk | 1.0–1.2 | Variable by application | 1.5–2.0 |
| ABL tube compatibility | ⚠️ Risk of delamination | ✅ Works (foil layer heated) | ✅ Preferred method |
| Heat-sensitive formulation safety | ❌ Conducted heat risk | ⚠️ Depends on foil proximity | ✅ Product zone unaffected |
| Energy draw model | Continuous (1–3 kW constant) | Duty-cycle at coil station | Duty-cycle only (lowest average) |
| Batch digital logging | Manual or basic log | Available on advanced systems | Full per-cycle digital record |
| Equipment cost range | $3,000–$35,000 | $20,000–$60,000+ | $15,000–$80,000+ |
| Consumables / wear parts | Heating elements, jaw surfaces | Coil replacement, foil stock | Sonotrode (3–5M cycles) |
Your Next Step: Eliminate Seal Risk With a Structured Decision
The decision to upgrade your sealing technology does not need to be complicated. It needs to be structured — based on your specific production data, your tube materials, and your compliance obligations — rather than based on catalog comparisons or vendor claims.
Here is a practical path from this guide to a production decision:
1. Run Your Own Numbers
Calculate your current annual scrap cost: (daily production volume × defect rate × material + fill cost per tube × 250 production days). Add rework labor at your actual labor rate. Add downtime costs at your actual contribution margin per production hour. This single calculation typically generates the business case for the technology evaluation without any additional analysis.
2. Send a Material Sample
Before specifying any equipment, send your actual tube material — the specific laminate construction, wall thickness, and diameter you are running — to the supplier for a sealing trial. Request a written compatibility report with seal strength data (ASTM F88 peel test), Cpk value from the trial run, and recommended process parameters. This is a standard pre-sale service from reputable suppliers; any supplier who declines or charges for it should be evaluated carefully.
3. Specify for Your Full Format Range
If you run multiple tube formats, confirm that the machine platform covers your full diameter range with appropriate tooling, and request documented changeover procedures and time estimates for each format transition. A machine that handles your primary tube but requires 90 minutes to change over to your secondary format has a hidden productivity cost that needs to be factored into the TCO comparison.
4. Lock in the Performance Guarantee
Specify a Factory Acceptance Test against your tube materials as a shipment condition — with agreed acceptance criteria for seal strength, Cpk value, cycle time, and energy consumption. This converts a supplier’s performance claims from marketing language into contractual commitments you can verify before the machine leaves the factory.
For distributors and agents: the tube packaging machine efficiency optimization guide from Miyoda Packaging Machinery covers the full range of sealing technology comparisons, line integration considerations, and performance monitoring frameworks — useful context for advising clients on equipment selection decisions across different production scales and compliance requirements.
Ready to Test Ultrasonic Sealing on Your Tube Material?
Miyoda Packaging Machinery works directly with cosmetic and pharmaceutical tube manufacturers and with equipment distributors to provide material compatibility testing, production trial support, and application-specific equipment configuration — before any purchase commitment.
Learn About Our Ultrasonic Sealing Solutions View Tube Filling & Closing Machines
Frequently Asked Questions
Answers to the questions cosmetic and pharmaceutical tube producers — and their equipment agents — ask most often about ultrasonic sealing technology.
1. How does ultrasonic sealing compare to thermal or induction sealing for soft tubes?
Ultrasonic sealing generates heat internally at the molecular layer interface — not conducted from an external jaw surface. This makes it faster (0.5–2 second cycle vs. 2–4 second thermal dwell), more consistent (Cpk 1.5–2.0 vs. 1.0–1.2 for well-maintained thermal equipment), and safer for ABL tube formats where external heat risks delaminating the aluminum barrier layer. Induction sealing is also effective for ABL tubes but requires a metallic foil layer positioned correctly for inductive heating — a construction requirement that ultrasonic sealing does not impose. For plastic-only tube formats, ultrasonic sealing is the superior option on both speed and consistency grounds.
2. Can it handle different tube diameters and thicknesses?
Yes — a correctly specified ultrasonic sealing platform covers a tube diameter range of approximately 16–60mm with sonotrode tooling matched to each tube format. Tooling changes between significantly different diameters typically take 15–30 minutes with documented changeover procedures. For most cosmetic and pharmaceutical tube portfolios (19mm–50mm is the common range), one machine platform covers the full range. Confirm that the supplier provides validated tooling for each tube format you run — not just the primary format — before finalizing the specification.
3. Is ultrasonic sealing suitable for sterile pharmaceutical packaging?
Yes — the contact-only, no-residue, no-fume process is well-suited to cleanroom-compatible and GMP-compliant pharmaceutical production environments. The equipment can be configured with stainless steel product-contact surfaces, IP65 or higher enclosure ratings for cleanability, and digital batch recording compliant with FDA 21 CFR Part 11. Confirm IQ/OQ/PQ documentation availability with the supplier before purchase — for pharmaceutical production, this documentation must be confirmed as an available deliverable, not a post-purchase service request.
4. What maintenance does an ultrasonic sealing machine require?
Routine maintenance is minimal compared to thermal sealing equipment. Daily: clean the sonotrode contact face and inspect for wear marks; verify cycle counter against the sonotrode replacement schedule. Weekly: check pneumatic pressure settings; run a five-tube quality check against specification. Monthly: full calibration verification; measure sonotrode wear against replacement threshold. Annually: complete mechanical and generator electronics inspection. Annual maintenance cost typically runs 2–4% of equipment value — lower than the 4–7% typical for conventional heat sealing equipment with more frequent wear-part replacement cycles.
5. Do I need to modify my existing filling line to integrate an ultrasonic sealer?
For standalone semi-automatic configurations — where operators hand-load filled tubes into the sealing fixture — no modification to the filling line is required. For inline automatic integration, the sealing station is conveyor-fed from the filler’s discharge, which typically requires a mechanical transfer section and an electrical interface for speed synchronization. The two integration parameters to confirm before purchase are: (1) your filling machine’s tube discharge pitch, and (2) your facility’s available electrical supply specification (voltage, phase, frequency). Both are routine integration parameters that experienced ultrasonic sealing suppliers resolve as part of a standard installation scope.
6. How much energy does an ultrasonic tube sealer consume?
Ultrasonic generators for soft tube sealing applications typically draw 500–1,000W during the active weld cycle (0.5–2 seconds per tube), then drop to near-standby current between cycles. In contrast, a conventional electric hot-jaw sealer maintains 1–3 kW continuous draw to keep the jaw surfaces at operating temperature, regardless of whether a tube is in the sealing station. The average energy consumption per sealed tube is substantially lower for ultrasonic equipment — published analysis documents 30–50% reduction in energy per seal at comparable throughput. On a multi-shift operation, this difference translates to a measurable quarterly utility cost reduction.
7. Can ultrasonic sealing close ABL tubes without damaging the aluminum barrier layer?
Yes — and this is one of the strongest technical arguments for ultrasonic sealing in ABL tube production. Conventional thermal sealing of ABL tubes risks delaminating the aluminum foil from the adjacent plastic layer, because the conducted heat from the external jaw must pass through the outer plastic layers and through the aluminum before reaching the inner sealing layer. The differential thermal expansion between the aluminum and the plastic creates stress at the interface. Ultrasonic sealing bypasses this entirely — the energy is deposited at the inner polymer layer interface directly, with no thermal stress to the aluminum layer or the laminate structure above it.
8. What is the lifespan of the sonotrode and transducer?
Sonotrode service life varies by application intensity: on standard cosmetic laminate tubes at production rates of 40–60 tubes per minute, typical sonotrode replacement intervals are 1–3 years, corresponding to 3–5 million seal cycles. Replacement cost ranges from $300–$1,500 depending on sonotrode specification and size. Transducers (the piezoelectric element driving the sonotrode) reliably exceed 5-year service lives with proper care, and in many installations have operated for 8–10 years without replacement. Confirm both replacement interval benchmarks and replacement lead times with the supplier before purchase.
9. Is operator training difficult for ultrasonic sealing equipment?
No. The operator interface on production-grade ultrasonic sealers presents a touchscreen showing the active recipe, a cycle status indicator, and fault messages with guided corrective actions. Operators do not control the sealing physics directly — they select the recipe, start the cycle, and monitor the status display. Most operators reach full production proficiency on a semi-automatic configuration within one to two supervised production shifts. Inline automatic configurations require two to four days of training to cover line integration, minor fault recovery, and the preventive maintenance schedule — not because the sealing operation is complex, but because there is more system to learn.
10. How do I confirm my tube material is compatible with ultrasonic sealing?
Send actual tube samples — your specific tube construction, wall thickness, and diameter — to the supplier for a sealing trial before any purchase commitment. A credible supplier will run sealed samples using your material, provide ASTM F88 peel strength data from the trial, confirm Cpk value from the test run, and recommend process parameters for your production setup. This pre-qualification service should be offered as a standard part of the sales process at no charge — any supplier who declines or charges for a material compatibility trial is structuring the relationship incorrectly from the start.
11. Can ultrasonic sealing handle high-viscosity products like thick gels or ointments without spillage?
Yes — and the fast cycle time is actually an advantage here. Thick gels and dense pharmaceutical ointments create backflow risk during sealing: as the sealing jaws close, product can be pushed upward toward the seal zone. Ultrasonic sealing’s typical cycle time of 0.5–1.5 seconds (vs. 2–4 seconds for thermal dwell) minimizes the window for product migration into the seal zone. Confirm the tube’s headspace above the fill level with the ultrasonic sonotrode contact zone — adequate headspace between fill line and seal zone is the primary design parameter for eliminating product contamination in the seal area, regardless of sealing technology.
12. Do ultrasonic sealing suppliers offer support for international distributors and agents?
The leading suppliers in this segment — those specifically serving the cosmetic and pharmaceutical tube packaging market — provide technical documentation packages, remote diagnostic access, spare parts logistics support, and application-specific configuration guidance for regional distributors. Before entering a distribution agreement, confirm: (1) spare parts lead times for the top 10 wear components in your region; (2) whether remote diagnostic access is available to you as a distributor (not only to the end customer); and (3) whether co-branded technical documentation is available for client presentations. These specifics distinguish a genuine distribution partnership from a transactional reseller arrangement.
13. What is the typical ROI timeline for an ultrasonic sealing investment?
Payback periods of 3–8 months are the documented range for mid-to-large cosmetic and pharmaceutical tube producers with current defect rates above 1.5%. The calculation has four primary inputs: scrap material saving (current defect rate minus 0.3%, times material cost per tube, times annual production volume), rework labor saving, throughput gain value (from faster cycle times), and energy cost reduction. Running those four calculations against your actual production numbers before any supplier conversation gives you the business case — and ensures that the equipment investment decision is based on your numbers, not a supplier’s template ROI model.
14. Can the system be upgraded later as production volume grows?
Yes — the modular architecture of modern ultrasonic sealing platforms allows a business to step from a semi-automatic standalone configuration to a fully inline automatic setup by adding the infeed and discharge automation modules to the existing sealing core, rather than purchasing an entirely new machine. This upgrade represents approximately 30–50% of a full new-system cost and allows production capacity to scale incrementally with volume. Confirm at the time of initial purchase whether the specific model you are buying supports this modular expansion path — not all platforms do, and discovering that limitation at the point of needing to scale is a costly constraint.
15. Is there any risk of overheating sensitive cosmetic or pharmaceutical formulations during ultrasonic sealing?
No — and this is the physics-based advantage that makes ultrasonic sealing particularly valuable for premium cosmetic and pharmaceutical applications. The heat generated during an ultrasonic cycle is confined to the molecular interface between the tube’s inner plastic layers at the seal zone. The product column above the seal zone remains at ambient temperature throughout the cycle. Independent stability testing on standard 35–50mm diameter cosmetic tubes has consistently shown no measurable temperature increase in the product zone during properly executed ultrasonic sealing cycles. For formulations containing heat-labile actives — retinol, vitamin C, certain antibiotics — this is a documented production process advantage, not a theoretical one.
Start With Your Actual Tube Material — Not a Catalog Comparison
The fastest path to a confident sealing technology decision is a compatibility trial using your actual tube construction and fill material. Miyoda Packaging Machinery provides pre-purchase material testing, documented performance reports, and application-specific machine configuration for both direct manufacturers and regional distributors — globally.
Explore Our Ultrasonic Sealing Guide View Tube Filling & Closing Machines















