
The Hidden Cost of Suboptimal Sealing Performance
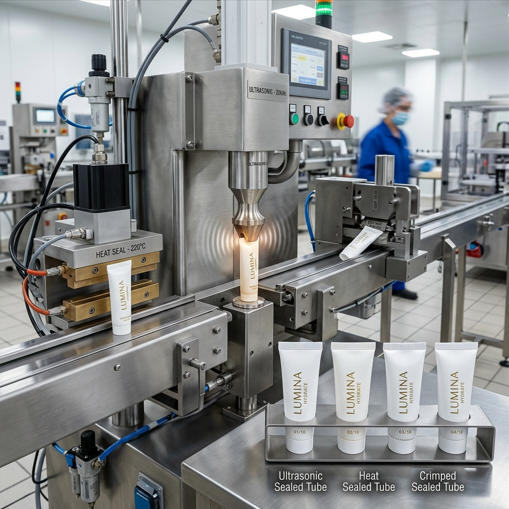
An ultrasonic tube sealer is one of the most precision-capable pieces of equipment on a cosmetic or pharmaceutical tube packaging line. It generates a hermetic seal through molecular fusion in under two seconds, with no external heat, no consumables, and seal consistency that thermal sealing simply cannot match. But that precision is only realized when the machine is operated, maintained, and monitored to the standard the technology is designed to deliver.
Most facilities don’t get there. Not because the machine is wrong — but because the process around the machine hasn’t caught up to it.
This guide is written for manufacturers, production managers, distributors, and agents who already have ultrasonic sealing capability — or are evaluating it — and want to extract its full potential. The five tips below are not theoretical. They are the specific operational practices that separate a line running at 78% OEE from one running at 94%.

OEE (Overall Equipment Effectiveness) on a well-run ultrasonic sealing line typically runs 92–96%. Getting there requires process discipline, not just equipment investment.
Implement a Daily Pre-Operational Seal Integrity Checklist
The problem this solves: Gradual quality degradation that becomes visible only after a batch has failed — not before it could have been prevented.
Ultrasonic sealing systems degrade progressively, not suddenly. A horn that is 0.04mm out of alignment today will produce seals that are visually acceptable but structurally marginal — seals that will fail a burst-pressure test or develop micro-leaks during distribution. By the time the problem surfaces in your end-of-line inspection or, worse, at a retailer, you’ve already produced several thousand compromised units.
A structured pre-shift check, taking 10–12 minutes per station, catches these developing issues before they become production events. Here is what the checklist needs to cover:
- Horn (sonotrode) alignment and contact face condition: Inspect the working face under bright light for uneven wear marks, pitting, or product residue from the previous shift. A horn with uneven wear delivers uneven amplitude across the seal width — the left side of the seal might be fully fused while the right side is under-bonded. Catch this at startup, not mid-batch.
- Anvil (lower sealing fixture) surface condition: The anvil provides the counter-pressure surface against which the horn works. Wear grooves or product build-up on the anvil surface create pressure voids in the seal. Clean with approved solvent and inspect for dimensional wear against the specification limit.
- Amplitude calibration verification: Run the system at your current recipe’s amplitude setting and verify the actual amplitude reading on the generator display matches the setpoint. A deviation of more than ±2% indicates a developing issue with the transducer or generator — flag it, don’t ignore it.
- Pneumatic pressure check: Confirm the air supply pressure reads within the specified range (typically 0.5–0.6 MPa for standard cosmetic laminate applications). Pressure variation directly causes trigger force variation, which causes seal width and depth inconsistency.
- First-tube production test: Run three tubes from your current production material, then perform a manual peel test on each. The peel behavior — clean layer separation at the bond zone — tells you more about seal quality in 30 seconds than any visual inspection of 100 tubes.
For pharmaceutical tube producers, this daily checklist serves a second function: it is the foundation of the pre-production equipment verification record that GMP-regulated facilities require before each batch release. Linking the checklist to your batch documentation system — even as a simple paper sign-off — creates the equipment-ready evidence that auditors look for.
A 10-minute pre-shift inspection catches the gradual degradation that becomes a 3-hour production stop — and a rejected batch — if left undetected.
Train Operators to Recognize Early Warning Signs of System Drift
The problem this solves: Unplanned downtime caused by issues that were detectable for hours — or shifts — before they caused a line stoppage or quality event.
Ultrasonic sealing systems communicate their condition continuously, if you know what signals to watch for. The problem in most facilities is that operators are trained to load tubes and respond to faults — not to monitor process health between faults. This gap converts early-warning signals into production emergencies.
Here are the specific signs that predict system drift, and what each signal means:
| Warning Sign | What It Indicates | Immediate Action |
|---|---|---|
| Seal appearance variation within the same batch — some seals look clean and flat; others appear slightly creased or translucent at the edge | Horn misalignment or uneven wear across the contact face. The center seals differently from the edges. | Stop production. Inspect horn alignment and contact face. Do not continue running on the assumption it will “even out.” |
| Unusual acoustic tone — the sealing cycle sounds slightly different from the normal crisp, short burst (harder to describe than to hear, but operators recognize it once trained) | Load resonance issue — the transducer stack is encountering unexpected mechanical resistance, often from product contamination at the seal zone or a loose joint in the horn-booster assembly. | Run a diagnostic cycle without a tube loaded. If the tone persists, check all mechanical joints in the stack for torque specification. Call your technician if the issue doesn’t resolve. |
| Generator power draw increasing — the wattage reading on the generator display is trending upward over a shift while output speed and amplitude settings remain unchanged | Increasing acoustic losses in the transducer stack, typically caused by wear in the piezoelectric ceramic elements or a developing crack in the booster or horn. | Flag for scheduled inspection at next maintenance window. If power draw exceeds rated capacity by more than 10%, inspect the stack immediately. |
| Cycle time lengthening — individual seal cycles are taking slightly longer than the recipe setpoint, measurable on machines with per-cycle timing displays | The generator is working harder to achieve the target energy delivery — a leading indicator of component wear before visible seal quality impact. | Record the trend over the shift. If cycle time has increased by more than 15% from the baseline, schedule a transducer inspection before the next production day. |
| Material charring or discoloration at the seal edge on laminate tubes | Amplitude is too high for the current tube material or wall thickness, or the dwell time is running long. The tube surface is absorbing more energy than the seal joint needs. | Reduce amplitude by 5% increments and re-test. Do not increase cooling time as a compensation — address the energy input directly. |
The most effective implementation of this training is a standardized shift logbook — physical or digital — where operators record one observation per hour: seal appearance (normal/marginal/flag), any acoustic changes, and any parameter deviations. This log has two functions: it creates a maintenance-relevant data trail for your technician, and it forces the observation habit that early-warning recognition requires.
Optimize Amplitude and Trigger Force Settings for Material-Specific Runs
The problem this solves: Weak seals on some tube formats and over-welding on others — both caused by running a single parameter set across materials that require different energy inputs.
Amplitude — the peak-to-peak travel distance of the sonotrode’s working face, measured in micrometers (µm) — is the primary energy input variable in ultrasonic sealing. Trigger force is the pneumatic clamping pressure that holds the tube tail between the horn and anvil during the sealing cycle. Together, these two parameters determine how much energy is delivered to the seal interface, and over what contact area.
The fundamental error is using one set of parameters across all tube formats. A 35mm PE laminate cosmetic tube with a 0.35mm wall thickness requires materially different settings from a 22mm ABL pharmaceutical tube with a 0.45mm wall — and running both on the same recipe produces one of two outcomes: over-welding on the thinner-wall tube (visible as material squeeze-out or surface marking) or under-bonding on the thicker-wall tube (seals that look complete but fail below burst specification).
Here is the practical framework for material-specific parameter optimization:
Start from a Known Baseline
Begin with your machine supplier’s recommended starting parameters for your tube material category (PE laminate, PBL, ABL). These are not production settings — they are your qualification starting point. Record them as the recipe baseline before any optimization begins.
Adjust Amplitude in 5% Increments
Increase or decrease amplitude in 5% steps — never more. After each adjustment, run five tubes and perform both a visual inspection and a manual peel test. Record seal width, peel behavior (cohesive vs. adhesive failure), and surface condition at each amplitude level.
Set Trigger Force to Match Wall Thickness
Thicker-wall tubes require higher clamping force to maintain full horn-to-material contact during the weld cycle. Standard PE laminate (0.30–0.40mm) typically runs at 300–400N clamping force. ABL structures (0.40–0.55mm) often require 450–550N. Confirm against your machine’s force-calibration specification, not just the pressure gauge reading.
Store Each Format as a Named Recipe
Once validated, store the optimized parameters as a named recipe — by tube SKU name, not by generic descriptor. “35mm PE Sunscreen” and “22mm ABL Antibiotic Cream” are more useful recipe names than “Laminate A” and “Laminate B” when an operator is switching between formats at shift changeover.
The acceptance criterion for a validated parameter set is quantitative, not visual. For cosmetic tubes, typical minimum peel strength is 15–25N per 15mm width (measured per ASTM F88 peel strength standard). For pharmaceutical tubes, minimum burst pressure typically exceeds 30N per ISO 11607 requirements. These thresholds should be documented in your process parameter record — not just “seals look good.”

Every tube material format requires its own validated parameter set. Running all formats on a single recipe is the single most common cause of inconsistent seal quality across SKUs.
Schedule Preventive Maintenance Based on Production Volume, Not Calendar Time
The problem this solves: Both over-maintenance (wasting budget on components that haven’t reached end-of-life) and under-maintenance failures (components that fail because a calendar-based schedule missed their actual wear rate).
A calendar-based maintenance schedule — “inspect the horn every three months” — is a proxy for what actually matters: how many sealing cycles has each component completed? A machine running two 10-hour shifts, six days per week accumulates maintenance triggers 4× faster than the same machine running one 5-hour shift, three days per week. A three-month interval that was adequate at one production level may become dangerously inadequate when volume increases.
The correct approach is cycle-count-based maintenance, using the machine’s cycle counter as the scheduling trigger. Here is the recommended maintenance interval framework for standard cosmetic and pharmaceutical tube sealing applications:
| Component | Maintenance Action | Recommended Interval | Consequence of Missing |
|---|---|---|---|
| Sonotrode (horn) contact face | Visual inspection + dimensional measurement against wear limit | Every 250,000 cycles (daily in high-volume facilities) | Uneven seal width; surface marking on premium tubes; seal strength below specification |
| Horn-booster-converter joint torque | Re-torque to specification using calibrated torque wrench (do not use power tools) | Every 500,000 cycles | Loose joints cause acoustic energy losses; hot spots in the stack; accelerated piezoelectric element wear |
| Piezoelectric converter (transducer) | Impedance measurement; cleaning of mating surfaces; inspect for cracking | Every 1,000,000–1,500,000 cycles, or at first sign of elevated generator power draw | Converter failure mid-production; typically 1–2 week lead time for replacement on fast delivery |
| Sonotrode replacement | Replace with new or reconditioned horn; re-tune generator to new horn’s resonant frequency | Every 3,000,000–5,000,000 cycles depending on material abrasivity | Over-worn horn delivers inconsistent energy; visible seal quality degradation that progresses rapidly once wear limit is exceeded |
| Pneumatic components (cylinders, fittings, pressure regulator) | Leak check; regulator calibration verification; O-ring inspection | Every 2,000,000 cycles or 6 months — whichever comes first | Pressure inconsistency; trigger force variation; seal width deviation between consecutive tubes |
| Generator electronics diagnostic | Full electrical diagnostic by certified technician; output frequency and power calibration | Annually, or after any electrical fault event | Generator delivering incorrect frequency to transducer; resonance mismatch causes heat build-up in the stack |
For high-output facilities — above 500,000 seals per month — predictive maintenance tools add a meaningful layer on top of this cycle-count framework. Modern ultrasonic generators with embedded diagnostics continuously monitor transducer impedance and flag developing issues before they reach the failure threshold. Some systems can be connected to IoT monitoring platforms that send maintenance alerts to a supervisor’s phone when a component is approaching its end-of-life cycle count — converting a reactive maintenance model into a genuinely predictive one.
Leverage Real-Time Monitoring for Immediate Feedback and Traceability
The problem this solves: Quality events that are discovered after they’ve already produced defective tubes — and compliance gaps that surface during audits rather than during production.
The most significant operational gap in most ultrasonic sealing installations isn’t hardware — it’s data. Modern ultrasonic generators capture per-cycle data: actual energy delivered (in joules), dwell time, trigger force, and cycle status (pass/abort). This data exists on the machine in every production cycle. The question is whether your facility is capturing, displaying, and acting on it — or letting it pass by unrecorded.
Here is what real-time monitoring delivers, practically:
Immediate fault detection: A generator configured with per-cycle pass/fail thresholds will flag and — on integrated lines — automatically eject any tube whose seal cycle fell outside the specified energy window. This converts your quality control model from statistical sampling (check 1 in 100 tubes) to 100% in-process screening. For pharmaceutical manufacturers, this is the difference between AQL sampling compliance and genuine process-level quality assurance.
Trend visibility before failure: When seal energy data is logged per cycle and trended over a shift, the gradient of change is visible before the threshold is crossed. A generator that was delivering 120J per cycle at the start of the shift and is now consistently delivering 108J — still within a ±15% tolerance band — is showing a 10% decline that, if unchecked, will cross the lower limit within the next two hours. Without data trending, this developing problem is invisible until the limit is crossed and tubes begin failing.
Regulatory audit readiness: For pharmaceutical manufacturers, FDA 21 CFR Part 11 requires that electronic records of manufacturing process parameters be attributable (linked to the operator who ran the batch), tamper-evident (change-controlled with an audit trail), and retrievable on demand. An ultrasonic generator with data logging capability, connected to your batch management system, satisfies this requirement automatically — each seal cycle is time-stamped, linked to the batch record, and retrievable without manual data entry.
Real-time monitoring converts seal quality data from a retrospective quality check into a live production control tool — and builds the audit trail that regulatory inspectors require.
Integration depth varies by facility. Entry-level implementations use the generator’s own data logging to a USB or SD card — reviewed at shift end, not in real time, but still a significant improvement over no data capture. Mid-level implementations connect the generator to a plant SCADA or MES (Manufacturing Execution System) via Modbus TCP or OPC-UA, enabling live dashboard visibility of all sealing stations. Advanced implementations integrate seal quality data with upstream fill-weight data — so a tube that received an under-fill AND an out-of-tolerance seal cycle is flagged through both data points for double-verification before it reaches the capping station.
The ultrasonic tube sealing guide for cosmetic and pharmaceutical manufacturers from Miyoda Packaging Machinery covers the full integration architecture options — from standalone semi-automatic configurations to fully integrated inline systems with real-time monitoring — and provides a practical framework for matching monitoring depth to production volume and regulatory requirements.
Watch: Ultrasonic Tube Sealing in Production
Seeing a sealing machine run on paper tells you the specs. Watching it run at production speed tells you the process. The following video demonstrates an ultrasonic tube sealing machine operating on cosmetic and pharmaceutical tube formats — pay attention to the seal cycle consistency, the tube handling behavior between stations, and the finish quality on the sealed tail:
Watch for cycle-to-cycle seal consistency, the acoustic behavior of the sealing cycle, and the finished seal tail geometry — these three points reveal production-level reliability.
Advanced Insight: How Seal Consistency Impacts Downstream Line Efficiency
Seal quality doesn’t stop at the sealing station. Every dimensional variation in the tube tail — a slight skew, a 0.5mm seal-width deviation, a tail that’s 1mm shorter on one side than the other — propagates downstream and causes problems at the next station in the line.
Here is what inconsistent sealing does to your downstream operations:
Labeling and Coding Errors
Tubes that exit the sealer with skewed tail orientation (a result of uneven horn pressure across the seal width) arrive at the label applicator and batch coder at inconsistent angles. A label applied to a skewed tube is positioned off-center — a cosmetic quality issue that triggers retail rejection for premium brands with ≤1mm label placement tolerance specifications.
Cartoning and Secondary Packaging Jams
A tube with a deformed or over-wide seal tail will jam in the cartoning machine’s tube-loading channel, which is dimensioned to the tube’s nominal tail width plus a clearance tolerance of 1–2mm. Even one jam event per 5,000 tubes on a line running 80 tubes per minute represents a stoppage every 62 minutes — a 1.3% downtime loss before any other sources are counted.
Vision Inspection False Rejects
Inline vision systems that inspect seal quality trigger on dimensional criteria — seal width, tail length, seal straightness. A sealing process with high natural variation generates a high false-reject rate from the vision system, even when the seals are structurally sound, because the variation falls outside the inspection tolerance. The result is a quality team reviewing and accepting rejected tubes manually — labor cost and lost throughput from a process problem, not a product problem.
OEE Impact
OEE (Overall Equipment Effectiveness = Availability × Performance × Quality rate) on a tube packaging line is a whole-line metric. A sealing process running at 96% quality rate — 4% rejects — constrains the entire line’s OEE ceiling to 96% regardless of how well every other station performs. Improving seal quality from 96% to 99.3% is the single change that most frequently moves whole-line OEE from the 78–82% range into the 92–95% range that world-class tube manufacturers achieve.
For a comprehensive framework covering all efficiency levers across a tube packaging line — not just sealing — the tube packaging machine efficiency guide from Miyoda Packaging Machinery covers the 10 highest-impact optimization steps across filling, sealing, coding, and downstream handling.
Value for Distributors and Agents: Supporting Clients with Expertise, Not Just Machines
If you represent packaging machinery in your region, the five operational tips above are also your most effective client retention tool. A client whose ultrasonic sealer is running at 94% OEE, with a documented pre-shift checklist and cycle-based maintenance schedule in place, is not a client who calls you with emergency support requests. They’re a client who reorders consumables, recommends you to peers, and asks about the next line expansion.
The client whose sealer is running at 79% OEE, generating recurring seal quality complaints, is a client who is quietly evaluating alternative suppliers — even if they’re not saying so.
Here is how distributors can translate the technical content in this guide into a structured client engagement:
Performance audit as a value-add service: Offer a half-day sealing performance audit to existing clients — bring the pre-shift checklist, the cycle-based maintenance framework, and a set of peel-test samples. Run the audit, document the findings, and present a structured improvement plan. This service costs you two to four hours of field time and delivers immediate, visible value. It also gives you a reason to be on-site at the client’s facility every quarter — which is more client contact than most competitors achieve in a year.
Spare parts kit recommendations: Based on the maintenance interval framework above, recommend a specific spare parts kit to each client: at minimum, one sonotrode at end-of-life threshold, one converter for inspection readiness, and common pneumatic wear items. Clients who hold recommended spares on-site recover from component failures in two hours rather than two weeks. Clients who recover quickly trust the equipment — and, by extension, the supplier who helped them prepare for the failure before it happened.
Operator training modules: Develop a two-hour operator training module based on Tip 2 — the early warning signs framework. Offer it as part of every new machine installation and as an annual refresher. Structured packaging machinery operator training directly reduces the frequency of avoidable machine damage caused by operators who recognize a warning sign but don’t understand its significance. It also positions you as the technical resource your client turns to for operational guidance — not just equipment sales.
Case Study: 28% Output Increase After Implementing Proactive Sealing Protocols
📋 European Cosmetic Tube Manufacturer — Laminate PE Tube Line
Starting situation: A mid-sized European contract manufacturer was producing approximately 22,000 tubes per shift on a fully automatic ultrasonic sealing line. Their end-of-line rejection rate was running at 2.3% — 506 rejected tubes per shift. Line stoppages from seal-related faults were occurring 3–4 times per week, averaging 45 minutes each. Total effective output was running at approximately 73% of the line’s rated capacity.
Root cause analysis: A structured audit revealed three overlapping problems: no pre-shift horn inspection protocol (early-stage horn wear was going undetected for entire shifts), a single set of amplitude parameters being applied to three different tube formats with wall thicknesses ranging from 0.28mm to 0.47mm, and no cycle-count-based maintenance schedule — maintenance was being scheduled by calendar month, which at that facility’s output rate meant the converter was being inspected at roughly 1.2 million cycles per interval rather than the recommended 1,000,000-cycle threshold.
Interventions applied:
- Pre-shift checklist implemented at both sealing stations (10-minute protocol, documented in the batch record)
- Amplitude and trigger force re-validated per tube format; three separate named recipes stored on the generator HMI
- Cycle-count-based maintenance schedule activated using the machine’s built-in cycle counter; maintenance alerts configured at 250,000-cycle intervals for the daily inspection and 500,000-cycle intervals for the joint-torque check
- Generator data logging activated; seal energy trend reviewed at each shift handover
Results at 90 days:
“The machine didn’t change. What changed was the process around it. We went from managing faults to preventing them — and the output numbers reflect that.” — Production Manager
This case study reflects a pattern that repeats consistently across facilities that implement structured operational protocols for ultrasonic sealing equipment: the largest single output gains come not from equipment upgrades, but from closing the gap between what the machine is capable of and what the process is currently allowing it to deliver.
Turn Your Sealer into a Strategic Asset
The ultrasonic sealer on your production line is engineered to seal tubes at low reject rates, with consistent dimensional quality, for thousands of hours of productive life. Whether it actually does that depends almost entirely on the five operational dimensions covered in this guide.
The pre-shift checklist catches the gradual wear that becomes a batch rejection. Operator warning-sign training converts a reactive fault-response model into a proactive prevention one. Material-specific parameter optimization eliminates the seal quality variance that a single-recipe approach generates across different tube formats. Cycle-count-based maintenance ensures components are serviced when they need it — not when a calendar says so. And real-time monitoring builds both the process visibility and the audit-trail documentation that regulated industries require.
None of these require a new machine. They require a structured process discipline applied consistently to the equipment you already have.
Ready to Close the Gap Between Potential and Performance?
Miyoda Packaging Machinery works with cosmetic and pharmaceutical tube manufacturers, distributors, and agents to implement the operational protocols that maximize sealing line output. Whether you’re evaluating new sealing equipment or optimizing an existing installation, our engineering team can assess your current setup and identify the specific improvements with the highest ROI impact.
Compare Automatic Tube Sealers View Tube Filling & Closing Machine
Frequently Asked Questions
Real answers to the questions production managers, quality teams, distributors, and agents ask most often about optimizing ultrasonic tube sealing performance.
1. How often should I inspect the ultrasonic horn and anvil for wear?
Visual inspection should happen at the start of every production shift — it takes 3 minutes and catches contact face wear before it starts producing off-specification seals. Dimensional measurement against wear limits should occur every 250,000 production cycles, or monthly — whichever comes first at your production volume. The 250,000-cycle trigger is more reliable than calendar time because it reflects actual mechanical wear rather than elapsed time regardless of production intensity.
2. What causes weak seals on aluminum-plastic laminate (ABL) tubes?
The four most common root causes, in order of frequency: (1) amplitude set too low for the ABL wall thickness — ABL tubes require higher energy input than equivalent-diameter PE tubes because the aluminum layer has different acoustic impedance; (2) contaminated sonotrode contact face — even a thin film of product residue reduces energy transmission to the seal interface; (3) trigger force set for a lighter-gauge tube format — ABL structures typically need 450–550N clamping versus 300–400N for standard PE laminate; (4) degraded converter performance — a converter past its inspection interval delivers less consistent energy per cycle, and the inconsistency often shows first on demanding materials like ABL rather than standard PE.
3. Can operator technique really affect sealing consistency?
On semi-automatic equipment, yes — significantly. The two most common operator-driven consistency issues are inconsistent tube loading depth (a tube loaded 2mm deeper than specification produces a seal positioned outside the intended tail zone, leaving a longer unsupported tail that can wrinkle during downstream handling) and variable loading speed (rapid placement can cause the tube to bounce on the fixture before the cycle starts, producing a momentary contact misalignment that results in a narrower seal on one side). On fully automatic equipment, operator influence is limited to setup and recipe selection — which is one of the main reasons fully automatic configurations achieve better Cpk values than semi-automatic at equivalent output volumes.
4. How do I know if my sealing parameters are fully optimized?
The definitive test is destructive: run peel tests (ASTM F88) and burst tests weekly on production-representative samples, and track the results on a control chart. When your mean peel strength is centered within the specification range and your standard deviation is low enough that the process Cpk exceeds 1.33, your parameters are optimized for the current tube format and material batch. If your peel strength mean is within specification but the standard deviation is high — meaning some tubes are near the upper limit and some are near the lower — you have a process centering problem (usually amplitude) rather than a process capability problem.
5. Is it necessary to recalibrate after changing tube size or material?
Yes, without exception. Each tube format — defined by diameter, wall thickness, and material structure — has a distinct optimal amplitude, trigger force, and dwell time. Running a previously validated parameter set on a different tube format without recalibration produces predictable results: either over-welding (if the new format requires less energy than the previous one) or under-bonding (if it requires more). The recalibration process — run five tubes at the new recipe starting point, perform peel tests, adjust in 5% increments, document the validated set — takes 45–90 minutes per format. It is time well spent.
6. What maintenance tasks should be handled in-house versus by a certified technician?
In-house (trained operators): daily sonotrode visual inspection, fixture surface cleaning, pneumatic pressure verification, and pre-shift seal quality test. These require training, not specialized tools. Certified technician: sonotrode dimensional measurement and replacement decision, converter impedance testing, generator frequency calibration, and electrical diagnostic work. The boundary is roughly “cleaning and observing” versus “measuring and replacing.” Crossing the boundary in either direction — operators attempting transducer testing with inadequate tools, or sending basic cleaning tasks to an external technician — wastes money and introduces risk.
7. How can I reduce seal-related downtime in high-speed production?
Three interventions with the highest ROI in high-speed environments: (1) implement cycle-count-based maintenance so components are serviced before they fail — every unplanned stoppage at 100+ tubes per minute costs 100+ tubes per minute of recovery time plus the investigation and restart sequence; (2) hold a validated spare sonotrode on-site, ready for swap — a horn change takes 20 minutes on a well-organized station; a horn sourced from a supplier takes 2–4 weeks; (3) activate real-time monitoring with fault alerts sent to a supervisor’s mobile device, so sealing faults are responded to in minutes rather than discovered at shift end during output count.
8. Are there compliance risks with inconsistent ultrasonic sealing in pharmaceutical packaging?
Yes — substantive ones. For pharmaceutical tube packaging, container closure integrity is a GMP requirement, not a quality target. Inconsistent sealing that produces seal strength variation below specification creates a documented out-of-specification (OOS) event under FDA 21 CFR Part 211. An OOS investigation requires root cause analysis, corrective action documentation, and potentially batch re-evaluation — all of which consume quality team resources and delay batch release. Repeated OOS events in seal integrity attract regulatory attention during inspections. The cost of maintaining consistent sealing is a fraction of the cost of managing its absence in a regulated environment.
9. Can ultrasonic sealing be used for multi-layer barrier tubes without damaging the structure?
Yes — with properly calibrated parameters. The key advantage of ultrasonic sealing for multi-layer structures (PBL, ABL, and EVOH-containing laminates) is that the energy is generated at the polymer-to-polymer interface of the inner layers, not conducted inward from the outside surface. This means the outer decoration layer, the aluminum foil in ABL constructions, and the EVOH barrier layer are not thermally stressed during the sealing cycle. The critical specification check is that your amplitude setting is validated specifically for the multi-layer structure you’re sealing — the energy input required differs from single-layer PE, and running the wrong parameters risks either insufficient fusion of the inner layers or acoustic stress cracking in the foil layer of ABL tubes.
10. What is the typical lifespan of an ultrasonic converter in tube sealing applications?
Under proper operating conditions — within rated amplitude range, adequate cooling, no mechanical overload events — a quality piezoelectric converter achieves 1.5 to 2 million cycles before inspection-indicated replacement. In practical terms for high-volume facilities, this translates to 12–18 months of service at two-shift production. Converters that are routinely operated at maximum amplitude, in high-ambient-temperature environments, or without scheduled stack inspections typically reach end-of-life significantly earlier. The leading indicator is rising generator power draw — when power draw increases by more than 10% at constant amplitude and speed settings, the converter should be inspected regardless of cycle count.
11. How do temperature and humidity affect ultrasonic sealing performance?
Both have measurable effects. High ambient temperature (above 30°C) reduces the viscosity of PE-based tube materials, which means the material at the seal interface softens more readily — requiring a slight reduction in amplitude or dwell time to avoid over-welding. High humidity (above 70% RH) can cause surface moisture absorption in some laminate tube constructions, which slightly increases the acoustic impedance of the interface and may require a minor amplitude increase to maintain consistent seal strength. Both adjustments are small — typically ±3–5% on amplitude — but facilities in regions with significant seasonal temperature and humidity variation should build seasonal parameter reviews into their recipe management process.
12. Is it possible to upgrade older ultrasonic sealers with modern monitoring capabilities?
In most cases, yes. The primary retrofit path is installing a digital generator in place of an older analog generator — modern digital generators from established manufacturers include per-cycle data logging, USB or Ethernet data output, and programmable amplitude profiles as standard features. The transducer and sonotrode from the existing machine are typically compatible with a new generator provided the frequency matches (20 kHz is standard; confirm before specifying a replacement). The retrofit cost — generator plus installation and tuning — typically runs 25–40% of the cost of a new machine, and delivers the data logging and monitoring capability of current-generation equipment without replacing the mechanical sealing structure that still has useful life remaining.
Want a Performance Assessment of Your Current Sealing Line?
Miyoda Packaging Machinery supports cosmetic and pharmaceutical tube manufacturers — and the distributors and agents who serve them — with application-specific sealing line assessments, parameter optimization support, and full technical documentation. Share your current tube format, production volume, and sealing challenges; our team will identify the highest-impact improvements for your specific operation.
Contact Miyoda Packaging Machinery Automatic vs Semi-Auto Sealer Guide















